About Color Sorter Machines
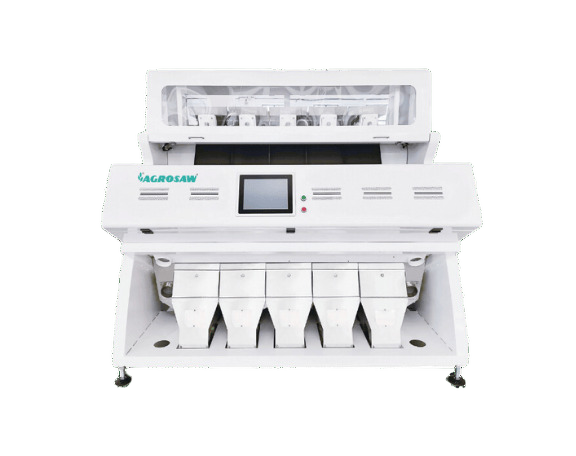
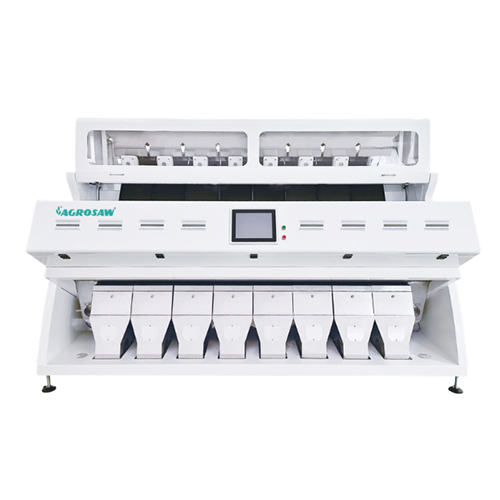
Discover extraordinary instant savings on our famed Color Sorter Machines-currently available at clearance prices with reduced rates like never before! Engineered for impeccable performance, these machines employ state-of-the-art CCD camera-based optical sorting and high-resolution full-color sensors for exceptional accuracy. The high-speed solenoid valve air jet ensures a low 0.2% rejection ratio, delivering 99% sorting efficiency. User-friendly touchscreen controls, stable LED illumination, and remote service support guarantee seamless operation. Tailored for distributors, exporters, importers, and manufacturers in India, these machines are ideal for rice, grains, pulses, plastics, and more.
Versatile Applications Across Diverse Industries
Color Sorter Machines are innovatively designed for a wide spectrum of industries. Their advanced sorting technology is crucial in food processing facilities for rice, grains, and pulses, as well as in plastics, recycling, and other granular product sectors. Renowned for both commercial and industrial usage, these machines assure unparalleled precision and quality control. From large warehouses to small-scale operations, their area of application covers nearly every setting that demands efficient, high-capacity sorting solutions.
Domestic and International Market Reach at Unbeatable Value
Our Color Sorter Machines are supplied at the lowest prices across the main domestic markets in India, with robust logistics ensuring swift order processing and delivery. Serving global export markets, we efficiently manage shipments from designated FOB ports for seamless international trade. Whether ordering a single unit or bulk volumes, clients benefit from prompt logistics solutions, steadfast support, and competitive pricing tailored for distributors, exporters, importers, traders, and manufacturers.
FAQ's of Color Sorter Machines:
Q: How does the CCD camera-based optical sorting technology operate in Color Sorter Machines?
A: The advanced CCD camera-based optical sorting technology analyzes each particle's color, shape, and size with precision. It then uses high-resolution full-color sensors and a high-speed solenoid valve air jet to accurately separate out defective or unwanted items, maintaining up to 99% sorting accuracy.
Q: What are the main application areas for these Color Sorter Machines?
A: These machines are ideal for sorting rice, grains, pulses, plastics, and various granular materials, making them indispensable for food processing, recycling, and material quality control across multiple industries.
Q: Where can Color Sorter Machines be installed for optimal performance?
A: Color Sorter Machines are suitable for installation in commercial processing plants, storage warehouses, and industrial facilities where sorting efficiency and large capacity handling are essential requirements.
Q: What is the typical process for order placement and logistics?
A: Clients can place orders directly through distributors or manufacturers, with logistics teams ensuring the fastest order processing and timely shipments from the designated FOB port, both within India and for export markets.
Q: What benefits does remote service support offer for users?
A: Remote service support ensures users receive technical assistance without delay, minimizing downtime and maximizing operational efficiency, which is vital for industrial-scale sorting operations.


 Send Inquiry

 Send Inquiry


